


KOBEX Co., Ltd.
MWCC Inc.
KOBEX Co., Ltd. (“KOBEX”) and MWCC Inc. (“MWCC”) announce that KOBEX is launching sales of the microwave solvent distillation recovery equipment*1 jointly developed by the two companies as the “CA-800M-01 Series.” Sample tests and preliminary trials are available for customers considering installation.
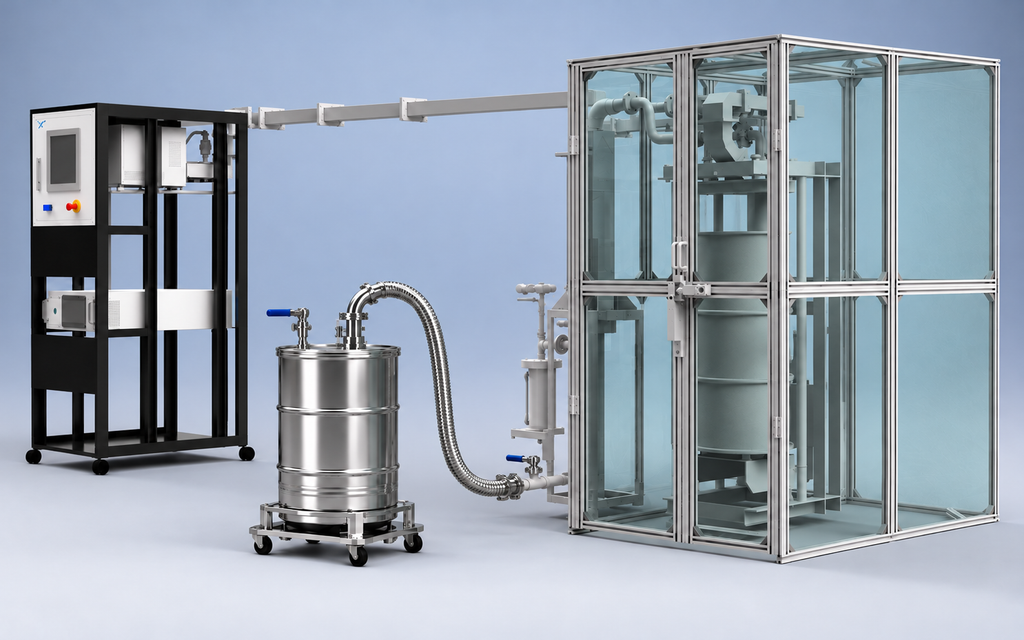
With a drum of spent solvent set in the unit as is, the equipment heats the solvent directly with microwaves to distill and recover it. It can be applied to solvents that were difficult to process with conventional heating methods, reducing the volume of waste liquid and turning solvents back into resources. This lowers both industrial waste disposal costs and the cost of purchasing new solvent, helping manufacturing sites achieve cost reduction and resource circulation at the same time.
【Background】
Organic solvents are widely used at manufacturing sites for cleaning and in various production processes. Used solvents can be reused as recycled solvent by separating out impurities through distillation. However, depending on the type of solvent and the contaminants it contains, conventional external heating methods have in some cases been unable to heat the solvent sufficiently, or processing has been hindered by residue adhering to heat transfer surfaces.
KOBEX has developed and manufactured solvent recovery equipment for organic solvent recycling for many years. MWCC has built up microwave heating technology that can supply energy directly to target materials, as well as know-how in implementing microwave technology in industrial processes.
Combining their respective expertise, the two companies began developing new distillation recovery equipment capable of handling spent solvents that were difficult to process with conventional methods, and announced the start of joint development in February 2026. Following the fabrication and verification of a prototype, the equipment has now been commercialized as the “CA-800M-01 Series” and is being launched.
【Features of the “CA-800M-01 Series” Microwave Solvent Distillation Recovery Equipment】
1. Direct processing of spent solvent in its drum
A 200 L drum can be set inside the unit as is for distillation. Since there is no need to transfer spent solvent into a separate vessel, the operator workload is reduced.
2. Direct heating with microwaves
Unlike conventional external heating methods, the equipment uses microwaves to heat the target material directly. This enables it to handle solvents that were difficult to heat sufficiently with conventional methods, while suppressing residue adhesion to heat transfer surfaces, which is expected to increase recovery volume. Thanks to improved heating efficiency, a distillation speed of 300% of conventional levels can also be achieved (depending on the solvent).
3. In-plant regeneration and reuse of spent solvent
Spent solvent that was previously disposed of as industrial waste can be distilled and recovered on-site and reused as recycled solvent.By turning solvent destined for disposal into a resource for reuse, the equipment reduces both new solvent purchases and industrial waste disposal volumes, promoting resource circulation at manufacturing sites.
【Intended Applications and Industries】
The equipment is intended for use across a wide range of manufacturing industries that use organic solvents, including paints and inks, resins (including synthetic resins), and chemicals and fine chemicals.
Sample tests and preliminary trials tailored to the properties of the target solvents and waste liquids are also available, supporting the introduction of solvent recycling suited to each manufacturing site.
【Outlook】
KOBEX will offer the equipment as a new addition to its lineup of solvent recovery equipment, contributing to resource circulation and reduced environmental impact for manufacturers facing challenges in treating and disposing of spent solvents.
By supplying microwave technology for this equipment, MWCC will advance the social implementation of its technology at manufacturing sites. MWCC will also accumulate insights gained through on-site operation and grow both its technology and its business, aiming to realize its vision of “Beyond Commercial Deployment.”
*1 Press release dated February 3, 2026 (issued under MWCC’s former name, Microwave Chemical Co., Ltd.)
“Development of Microwave Vacuum Solvent Distillation Recovery Equipment for Greater Energy Efficiency, Production Efficiency, and Capacity ― Utilizing the Features of Microwave Heating to Supply Energy Directly to Substances ―”
https://mwcc.jp/post_en/press_release/4326/
【Company Profiles】
KOBEX Co., Ltd.
Since its founding in 1969, KOBEX has been a comprehensive manufacturer of organic solvent recycling equipment, leveraging patented technologies to develop environmental and labor-saving equipment that meets the needs of the times. To date, the company has internally developed numerous solvent regeneration (recovery) units and various equipment related to organic solvents, delivering innovative products to its customers.
MWCC Inc.
Established in 2007. On October 1, 2026, the company changed its name from Microwave Chemical Co., Ltd. to MWCC Inc. MWCC is a deep-tech company that integrates research and development, engineering, and business development to turn its proprietary technologies into equipment operating in the field and into sustainable businesses. Through its microwave solutions business and other activities, it works to solve challenges in the energy and environmental fields by implementing its technologies in industry.